GPU环境技术
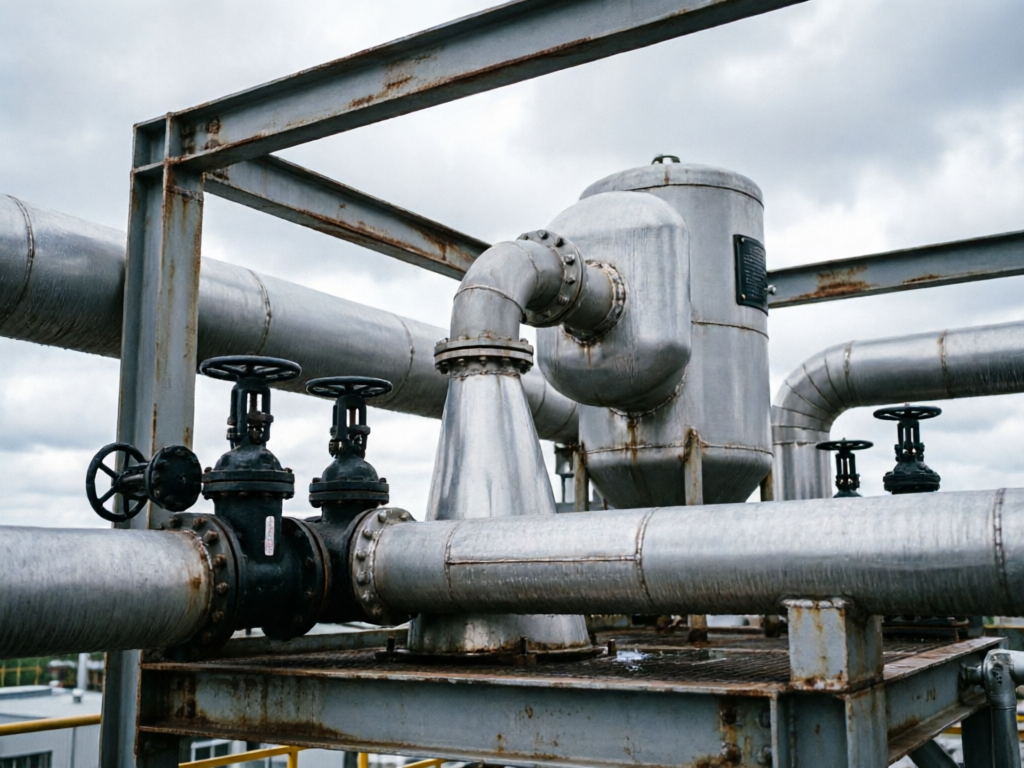
Blast furnace top gas recovery ejector system installed at a steel plant

Industrial Energy Saving Retrofit

Blast Furnace Top Gas Recovery Ejector System

GP-YSQ Series

Dry cleaning ejector train that returns blast furnace top pressure equalisation and bleed-off gas to the clean gas main instead of flaring it.

Recovery method
Dry cleaning plus ejector return
Recovery time
Designed per furnace volume and cycle
Buffer
Buffer tank to stabilise bleed pressure
Control
Interlocked with furnace PLC

Data needed for an accurate quotation

  • Air or gas volume at operating temperature
  • Dust or pollutant type and concentration
  • Required outlet concentration or standard
  • Available plot size and power supply

Technical parameters

Grouped specification sheet

Technical parameters
Performance
ApplicationTop pressure equalisation and bleed-off gas during bank and downtime
Recovery routeDry dust cleaning, then ejector return to the clean gas main
Recovery timeCalculated from furnace volume, bleed diameter and ejector capacity
Dust handlingCollected dust discharged dry through an airtight valve
Process equipment
EjectorSteam or gas driven, sized per bleed flow
Buffer tankVolume set to limit pressure shock on the clean gas network
Dry cleaningBag filter or cyclone plus filter stage
ValvesDust tight dampers and slide gates with tight shut-off
Control and safety
InterlockLinked to the blast furnace main control system
MonitoringCO, pressure, temperature and oxygen analysers
ProtectionExplosion venting and inerting points per site standard

Values shown are the standard manufacturing range. Final parameters are calculated from your gas volume, dust or pollutant load, temperature and the emission standard in force at your site.

Customisation options

  • Ejector and buffer volume sized from your furnace volume and bleed cycle
  • Material and lining selected for dust abrasiveness and gas temperature
  • Explosion protection and inerting arrangement per site safety standard
  • PLC integration with the existing furnace control system

Export packing & delivery

  • Ejector, buffer tank and filter shipped in sections with assembly marks
  • Valves, instruments and analysers packed in plywood cases
  • Process flow diagram, interlock list and commissioning sequence included

Drawings, assembly sequence, manual and test records are supplied with every shipment. On-site engineer dispatch can be arranged for complete system projects.

Read the export and installation checklist

Matched equipment

Systems usually supplied together

Collector, fan, discharge valve and conveying equipment designed as one train so interfaces and spares stay consistent.

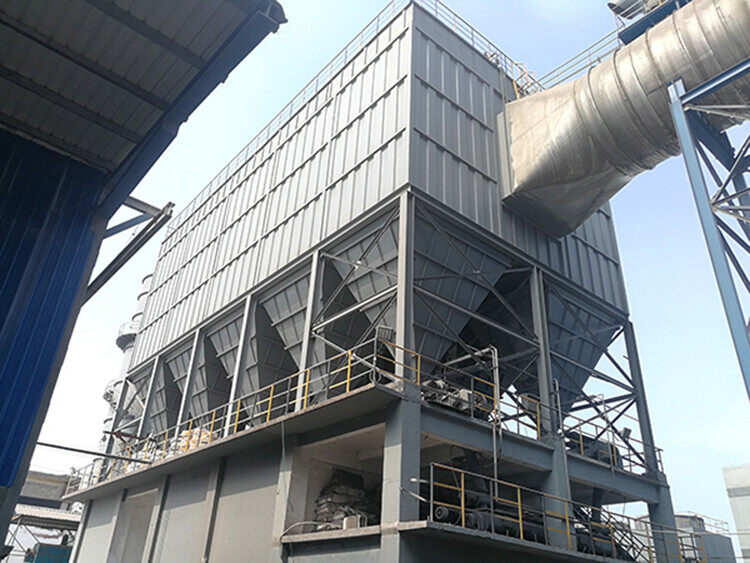
Multi-hopper pulse baghouse dust collector installed on a steel platform with top inlet duct

Industrial Dust Collection

Long Bag Offline Pulse Baghouse Dust Collector

GP-LCM / GP-PPC Series

Offline pulse jet baghouse for high dust load flue gas from sintering, blast furnace cast house, cement grinding and boiler tails.

Air volume
10,000 - 600,000 m³/h
Filter area
200 - 12,000 m²
Outlet concentration
≤ 10 mg/Nm³ (project dependent)
Operating temperature
≤ 260 °C with high-temp media
Industrial centrifugal induced draft fan with motor on a common base frame

Industrial Dust Collection

Industrial Centrifugal Induced Draft Fan

GP-4-73 / GP-9-19 Series

High pressure and high temperature centrifugal fans for dust collection, flue gas extraction and material conveying systems.

Air volume
5,000 - 400,000 m³/h
Total pressure
1,000 - 12,000 Pa
Motor power
7.5 - 1,250 kW
Gas temperature
≤ 450 °C with hot gas design
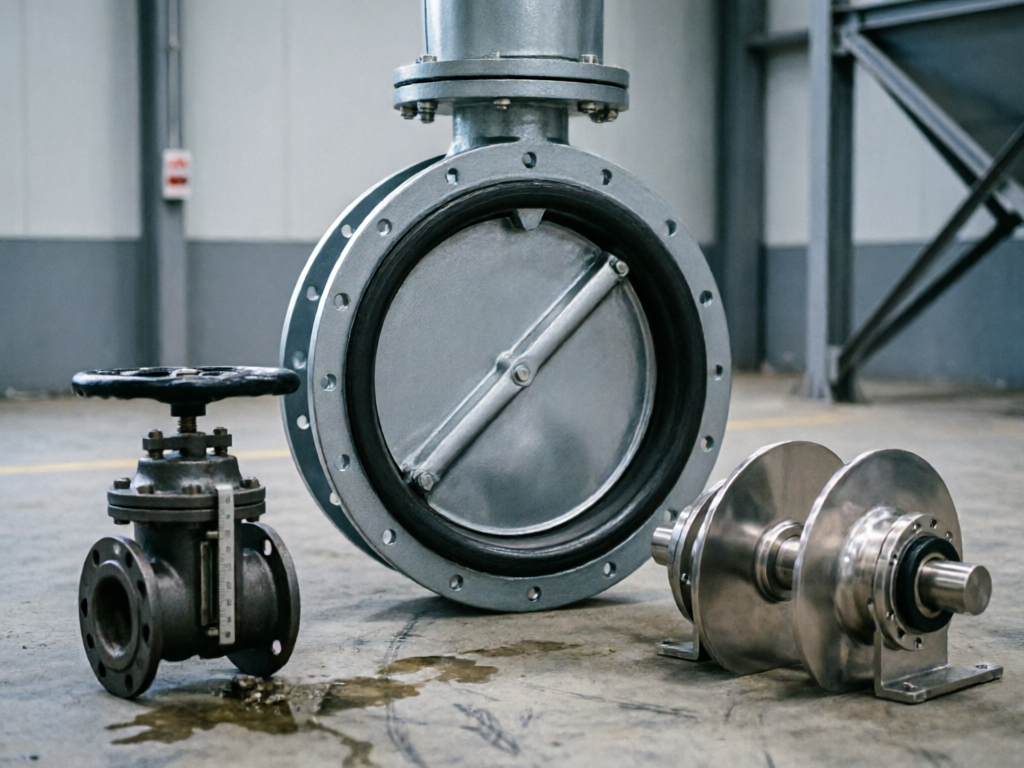
Industrial butterfly damper valve installed in dust extraction ductwork

Bulk Material Conveying

Duct Dampers, Slide Gate & Double Flap Valves

GP-VF / GP-CF / GP-DM Series

Butterfly and louver dampers, manual or pneumatic slide gates and double flap discharge valves for duct balancing and airtight hopper discharge.

Size range
DN200 - DN3000, square and round
Drive
Manual, pneumatic or electric
Temperature
≤ 450 °C depending on seal
Function
Balancing, isolation, airtight discharge
Variable frequency drive cabinet installed for industrial fan and pump energy saving retrofit

Industrial Energy Saving Retrofit

Fan & Pump VFD Energy Saving Retrofit

GP-VFD Series

Variable frequency drive retrofit for large induced draft fans, blowers and water pumps with throttling losses removed.

Motor power
15 - 2,500 kW
Voltage
380 V / 690 V / 3 kV / 6 kV / 10 kV
Typical saving
15 - 40% depending on load profile
Control
Local, remote, DCS or pressure/flow closed loop

Related technical articles

Selection notes for this equipment

Inquiry for Blast Furnace Top Gas Recovery Ejector System

The product name and model are attached automatically. Add your gas volume, dust or pollutant data and required outlet value.

Prefer a direct channel? Email szamtx@163.com or scan the WhatsApp QR code in the floating button.

Tell us your plant condition, we will size the system

Send air volume, dust or gas data, temperature and available space. Our engineers reply with a configuration proposal and a budget quotation within 1 working day.
我们仅使用必要的 Cookie 来维持网站运行,并记住您的语言设置和同意选择。不会设置广告或跨站跟踪 Cookie。阅读我们的 隐私政策.