Flue Gas Desulfurization & Denitrification
Boiler Flue Gas FGD and SCR Retrofit
Wet limestone-gypsum desulfurization tower with SCR reactor and wet electrostatic polishing added to an existing coal fired boiler flue gas train.
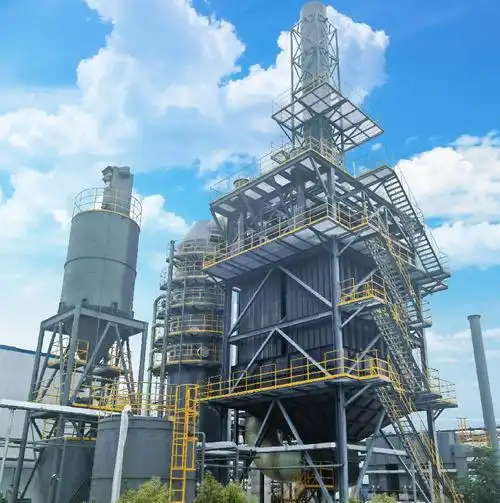
Original condition
The problem on site
The boiler had to keep running while the retrofit was built, the site had limited space behind the existing ESP, and the added system resistance exceeded the original induced draft fan margin.
Engineering approach
What we designed and built
- 01Designed a compact tower layout with the absorber and slurry tank arranged to fit the available plot, using a steel structure shared with the existing duct supports.
- 02Placed the SCR reactor in high dust arrangement upstream of the FGD to use the existing temperature window without reheating.
- 03Used three spray layers with a low pressure drop demister to keep total resistance within the upgraded fan capability.
- 04Retrofitted the induced draft fan and circulation pumps with medium voltage VFDs so the plant can follow load changes.
- 05Phased construction around planned outages, with bypass damper arrangement for start-up and maintenance.
Measured results
Before and after commissioning
Values recorded on this project under its own operating condition. Results at another plant depend on fuel, material, load profile and the local standard in force.
| Item | Before | After |
|---|---|---|
| Flue gas volume treated | Existing ESP only | 780,000 m³/h full train |
| SO₂ removal | No desulfurization stage | 96% removal at rated load |
| NOx removal | Combustion control only | 88% removal with SCR at 2 layers |
| Fan power after retrofit | Original ID fan margin | ID fan upgraded with VFD to cover added resistance |
Outcome
How the system runs now
The full train now handles 780,000 m³/h of flue gas. SO₂ and NOx removal rates measured during the performance test reached 96% and 88% at rated load, and outlet values are recorded by the plant CEMS. Final compliance is judged against the local emission limit and actual fuel quality.
Site records
Fabrication, erection and commissioning
Planning a similar retrofit or new build?
Send air volume, dust or gas data, temperature and available space. Our engineers reply with a configuration proposal and a budget quotation within 1 working day.